Manufacturing Record

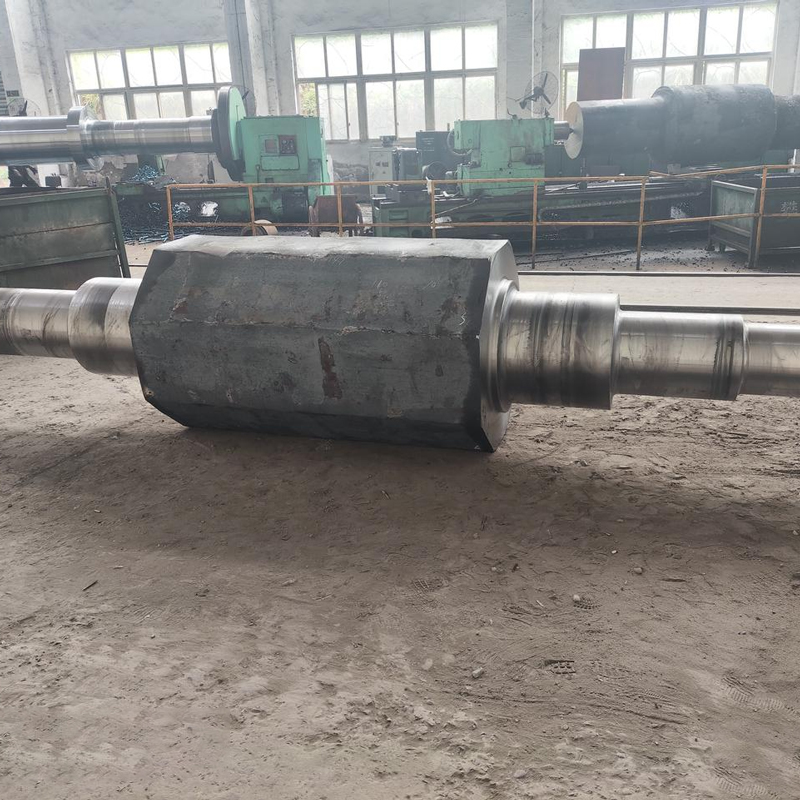
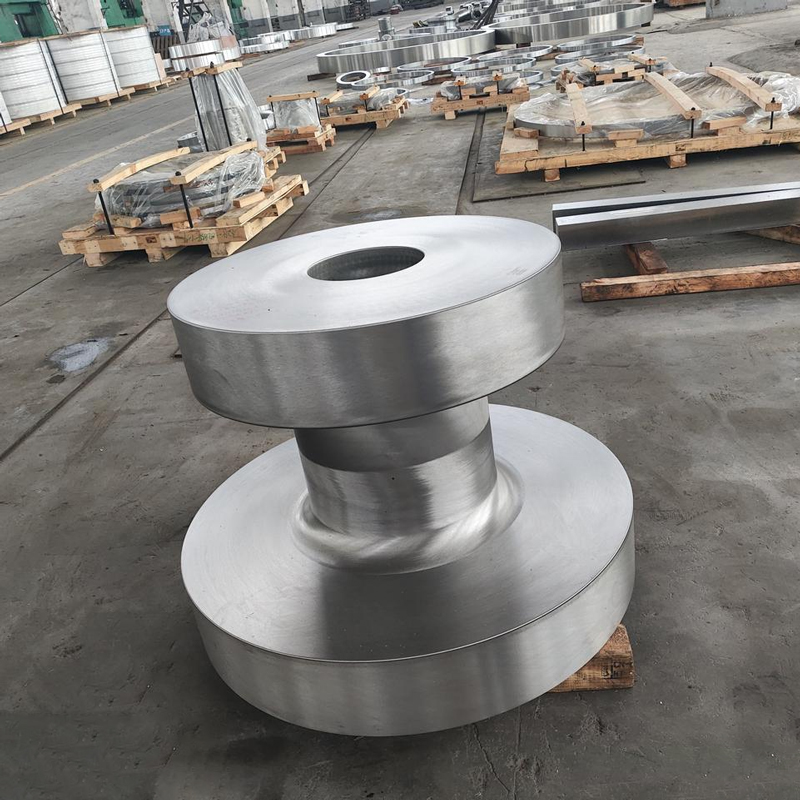
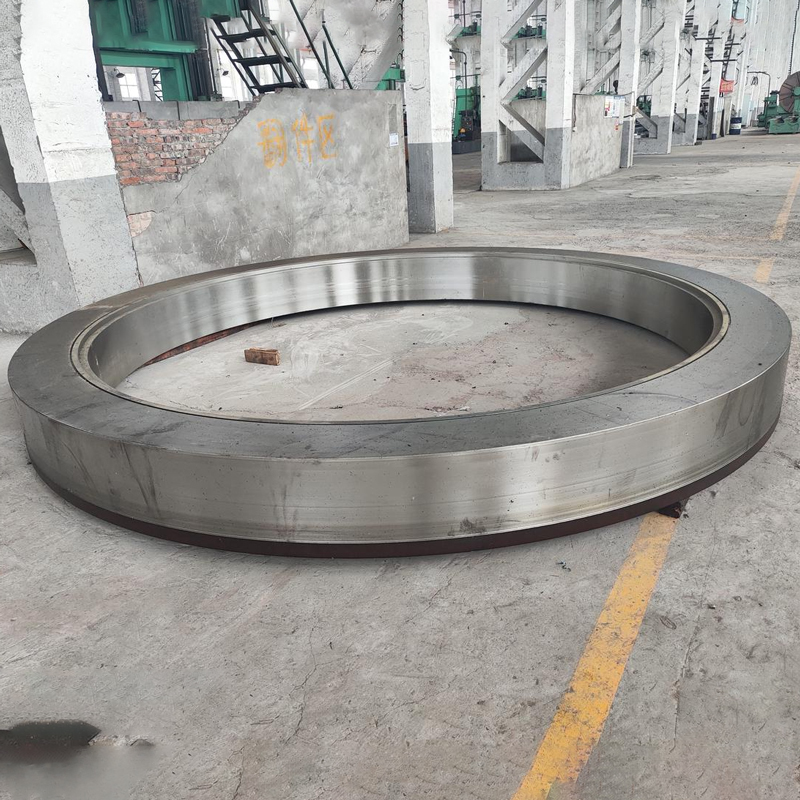
34CrMo1A Thermal-Power Rotor

A quenched-and-tempered rotor engineered for centrifugal force, alternating stress and high-temperature thermal-power operation.

Engineering case

Engineering challenge, manufacturing response and verified result

Component application, material and performance requirements are translated into defined manufacturing controls and documented verification.

01Project context
Component
34CrMo1A Thermal-Power Rotor
Dimensions & Weight
Project-specific

Application

Thermal, combined-cycle and biomass power units

Material

34CrMo1A alloy steel

Performance & acceptance points
  • Tensile strength >= 980 MPa
  • Yield strength >= 830 MPa
  • Elongation >= 12%; 260-300 HBW
02Engineering problem

Challenge

For Thermal, combined-cycle and biomass power units, the 34CrMo1A Thermal-Power Rotor must use 34CrMo1A alloy steel at project-specific dimensions and weight while meeting Tensile strength >= 980 MPa; Yield strength >= 830 MPa; Elongation >= 12%; 260-300 HBW. The engineering challenge is coordinated control of metal flow, section uniformity and internal integrity.

03Manufacturing response

Manufacturing Scope

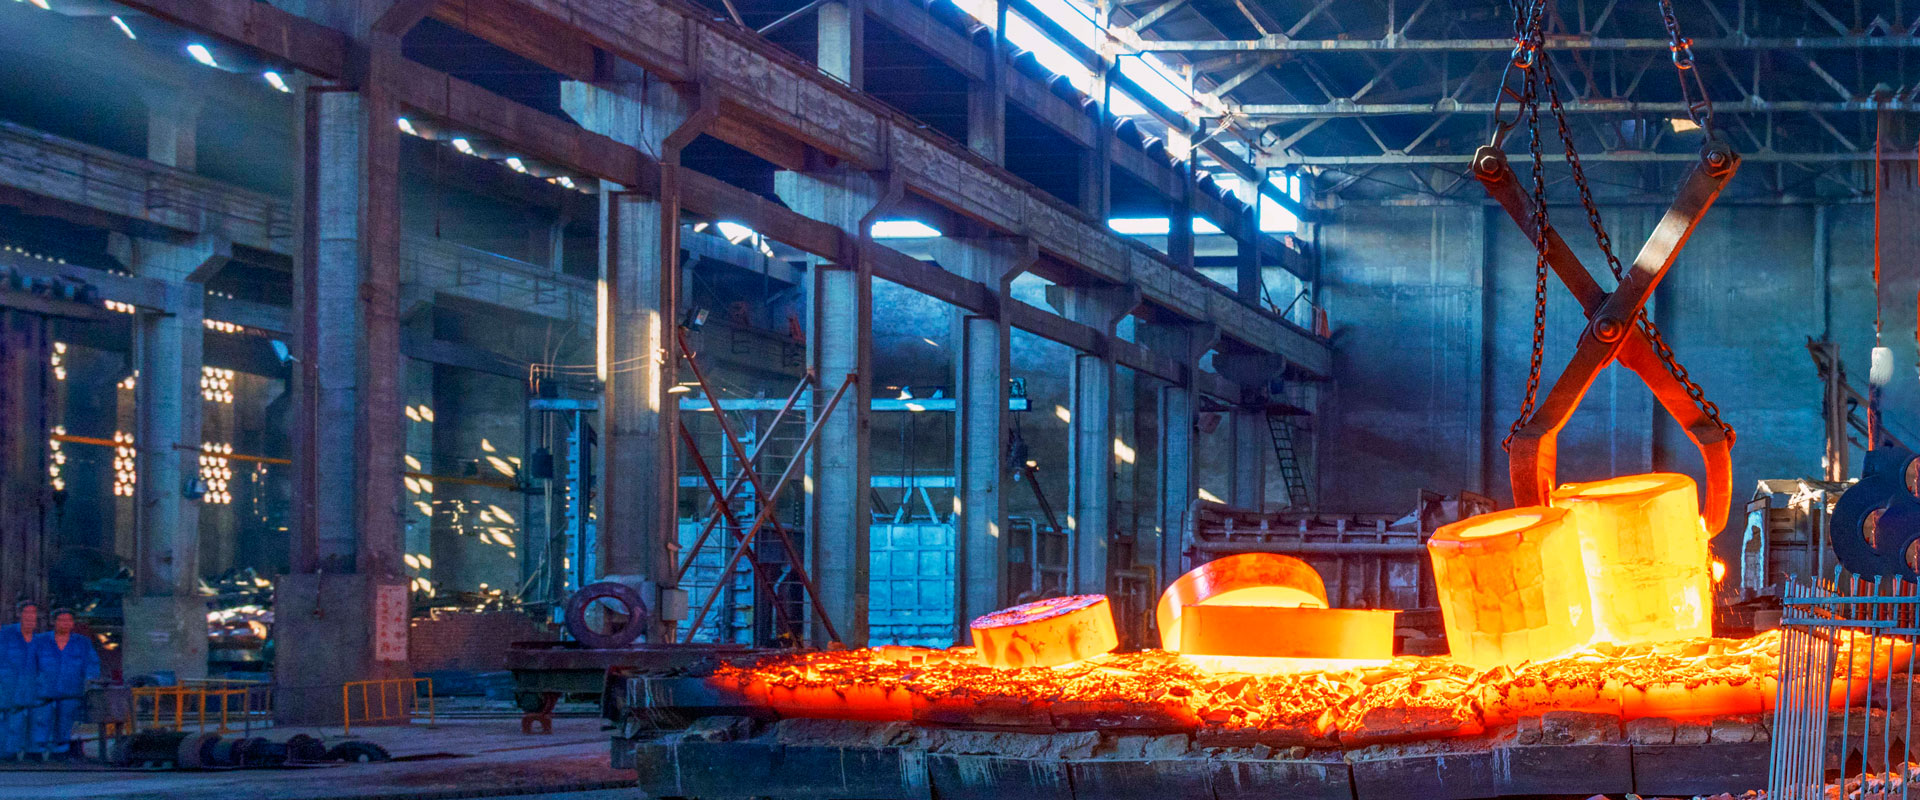
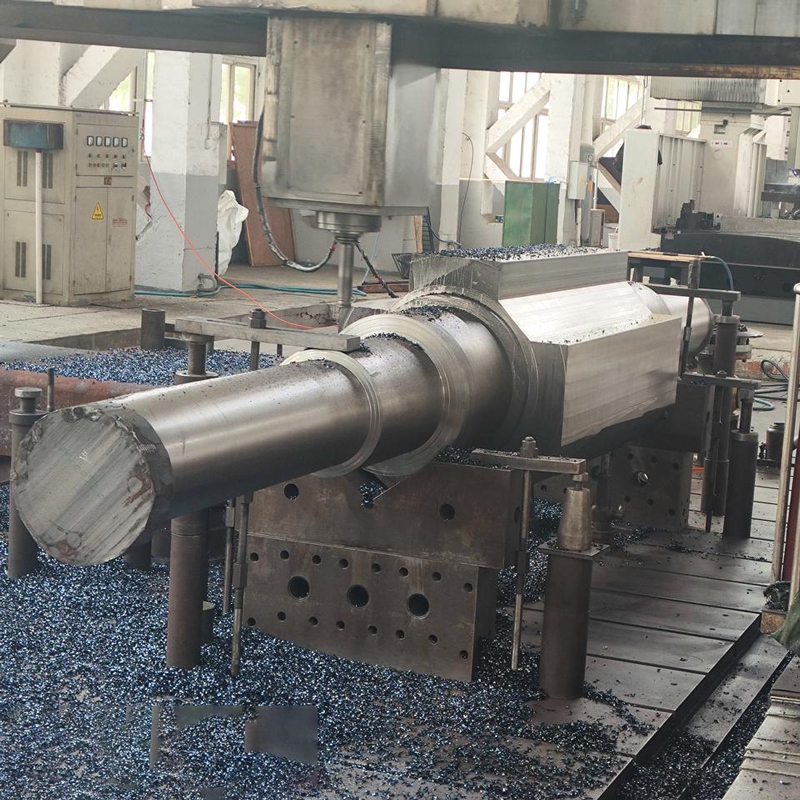
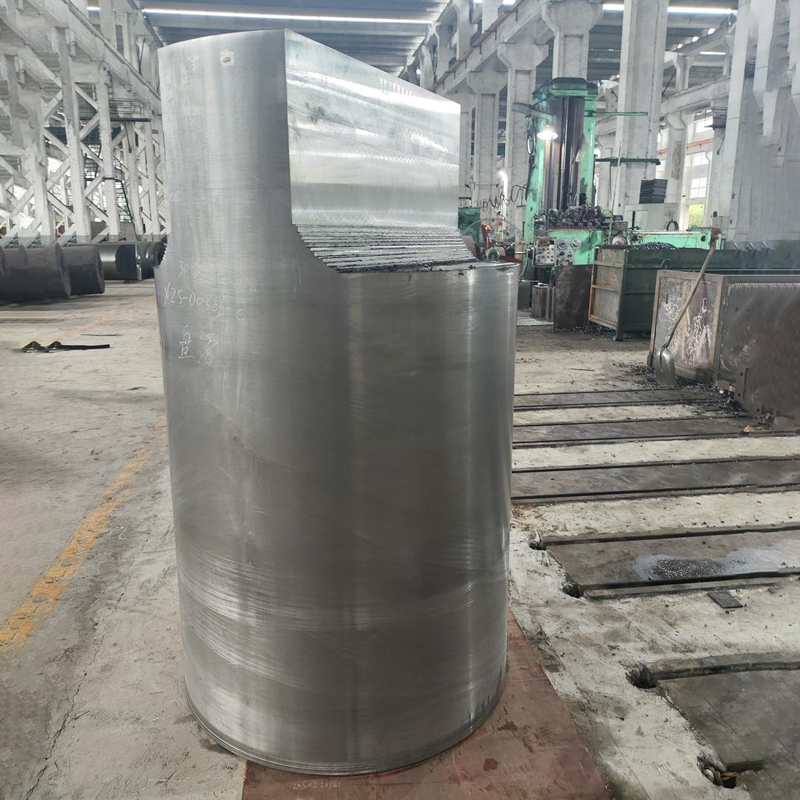
01Material & heat review02Heating & open-die forging03Post-forging heat treatment04Rough & finish machining05NDT & property testing06Final inspection & packing
Core Manufacturing Strategy

YL Solution

The forming strategy controls metal flow, section uniformity and internal integrity. Heating practice, deformation sequence, forging reduction, heat treatment and machining allowance are coordinated with defined material, dimensional, NDT and property release points.

Forming capabilityOpen-die hydraulic presses and project-specific tooling
Heat treatmentPost-forging heat treatment aligned to material and property targets
MachiningHeavy turning, milling and project-specific finishing
Inspection controlChemistry, mechanical properties, NDT and dimensional inspection
04Verified delivery

Result / Verification

Delivery basis: Machined condition. Tensile strength >= 980 MPa; Yield strength >= 830 MPa; Elongation >= 12%; 260-300 HBW are incorporated into the project inspection plan, with final inspection records and the quality dossier supporting acceptance and release.

Product technical recordParameters, inspection and delivery records
Material grade34CrMo1A alloy steel
Mechanical propertiesRm >= 980 MPa; Rp0.2 >= 830 MPa; A >= 12%; 260-300 HBW
Forging route8000 t-class hydraulic press; heating range 820-850 C
Machining referenceTurning tolerance +/-0.03 mm; grinding ovality <=0.005 mm; Ra <=1.6 um
Inspection plan

Spectrometric chemistry verification with elemental accuracy of +/-0.001%

UT and MT for internal and surface integrity

Mechanical testing up to the approved rotor specification

Delivery dossier

Material certificate and heat/lot traceability

Heat-treatment and inspection records

Final dimensional report and release dossier
Related products

Related manufacturing experience and products.

Engineering review

Submit drawings and requirements for this product.

Share drawings, material requirements or a development brief for an initial manufacturing-route and verification review.

Start an engineering review
LinkedInRequest a quote